
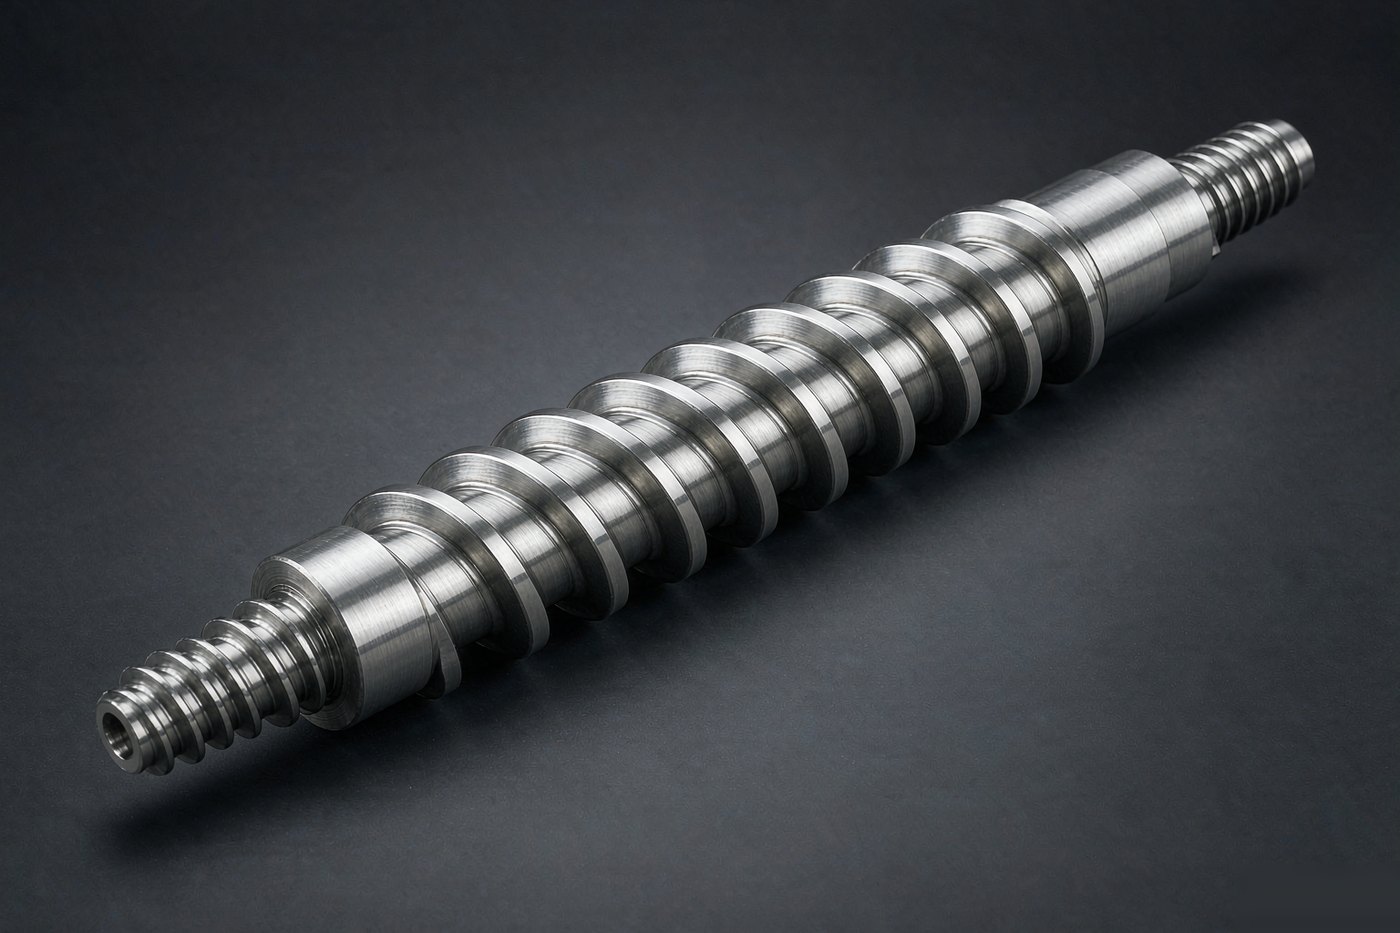
Injection Molding Screws — Nitrided & Bimetallic
Injection and extrusion screws in nitrided, bimetallic and hard-chrome finishes, cut to your barrel dimensions and screw geometry rather than to a catalogue number.
View details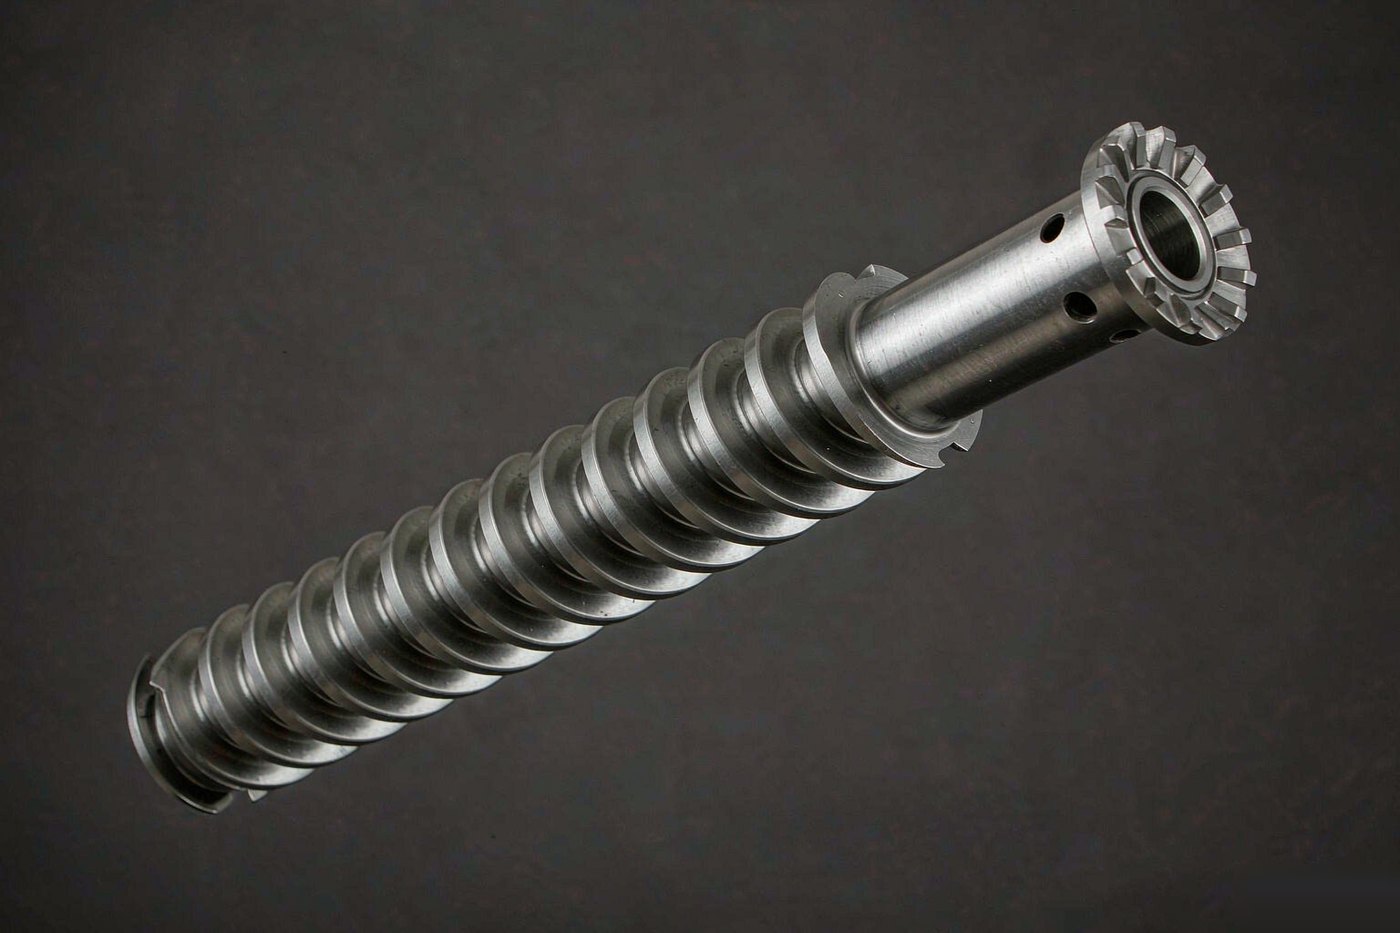
Adds a dispersive or distributive section to solve color streaks, specks and temperature variation.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
A mixing screw adds a dispersive or distributive element at the metering end. It is not a different way of melting — it is a way of homogenizing what has already melted, which is why it is usually specified on top of a three-zone or barrier profile rather than instead of one.
| Element | Mixing type | Best for |
|---|---|---|
| Pins | Distributive | Simple color and regrind blending; easy to clean |
| Maddock / slotted flight | Dispersive | Masterbatch agglomerates, filled compounds |
| Saucer or pineapple | Distributive with some shear | General homogenizing at moderate output |
| Static mixer in the nozzle | Distributive | When the screw cannot be changed but mixing must improve |
| Parameter | Typical range | Note |
|---|---|---|
| Mixer length | Usually 3 to 8 diameters | Longer mixing costs pressure and adds shear heat |
| Number of pins or slots | Set by the dispersion problem | More elements help dispersion but raise pressure drop |
| Channel depth in the mixer | Shallower than metering | Needs enough pressure to push melt through the restriction |
| Surface treatment | Same as the rest of the screw | Mixers wear at the flight tips first |
If the problem is unmelted resin rather than unmixed resin, a mixer will not help — it will just add shear heat to solids that never melted in the first place. Fix the melting length first.
Injection and extrusion screws in nitrided, bimetallic and hard-chrome finishes, cut to your barrel dimensions and screw geometry rather than to a catalogue number.
View details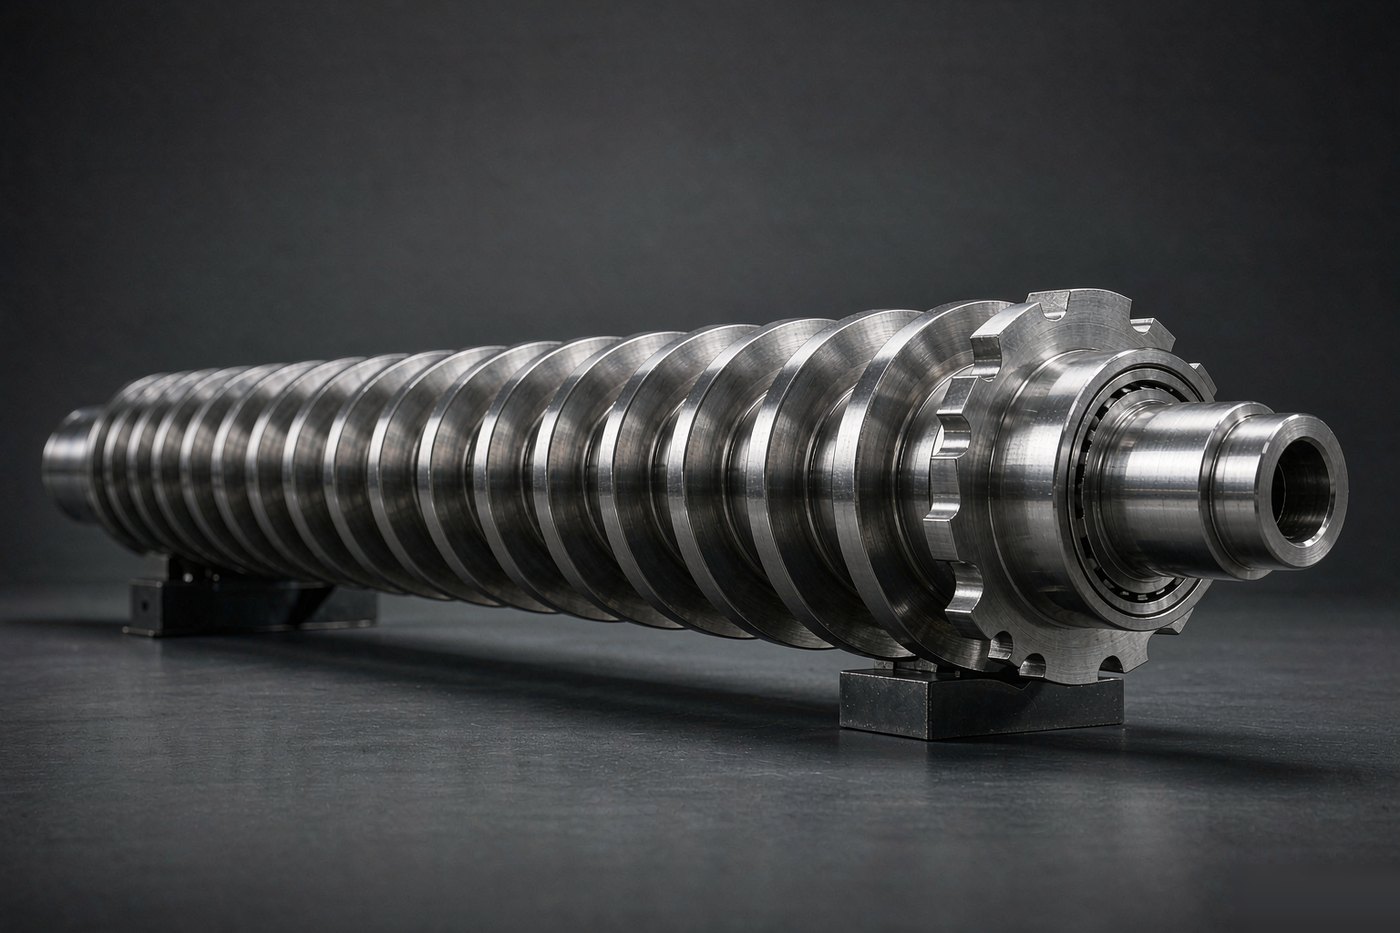
Separates solids from melt for a more even melt temperature on large shots and narrow processing windows.
View details
Three-zone screw for commodity and engineering resins where steady output matters more than dispersion.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.