
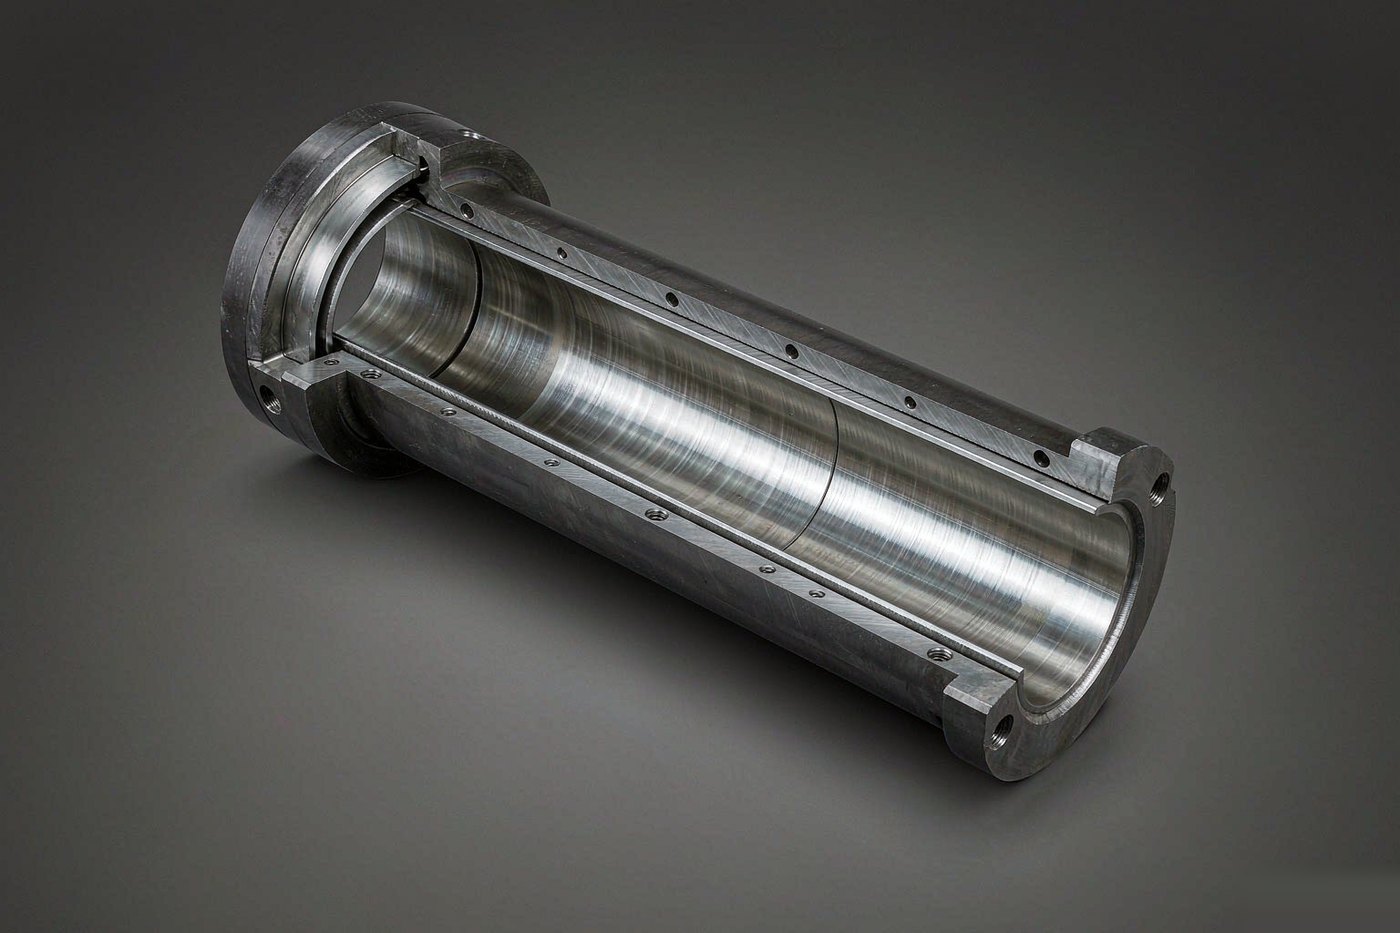
Bimetallic Barrel for Glass-Filled Compounds
Wear-resistant liner for glass-filled, mineral-filled and abrasive compounds.
View details
Barrels for injection and extrusion machines with nitrided or bimetallic liners, machined to your screw dimensions and inspected against drawing.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
Barrels wear from the inside, and the failure is quiet. A bore opens up by a few hundredths of a millimeter, the screw-to-barrel clearance grows, and the symptom is not a leak — it is a longer recovery time and a melt that will not hold pressure.
We machine barrels to your screw, or as a matched pair. The bore, the feed opening and the flange are cut to the machine interface you are bolting to.
| Type | How it is built | Where it fits |
|---|---|---|
| Solid nitrided | One piece 38CrMoAlA, nitrided through the bore | General purpose, unfilled resins; the economical choice |
| Bimetallic lined | Steel shell with a centrifugally cast alloy liner | Glass and mineral filled compounds, abrasive fillers |
| Vented | Two zones with a vent port and a decompression section | Moisture-bearing and regrind-heavy feeds |
| Grooved feed | Grooved throat section with a matched screw | Higher output on HDPE and PP, stable solids conveying |
A barrel is only half the pair. We set the bore-to-flight clearance against the screw we are supplying, and when you send an existing screw we measure the flights before cutting the bore. If only the barrel is being replaced, give us the screw diameter and the wear you have measured.
Bore tolerance, liner thickness and hardness are confirmed on the drawing for each order. The construction options above describe what we can make, not a stock specification sheet.
Wear-resistant liner for glass-filled, mineral-filled and abrasive compounds.
View details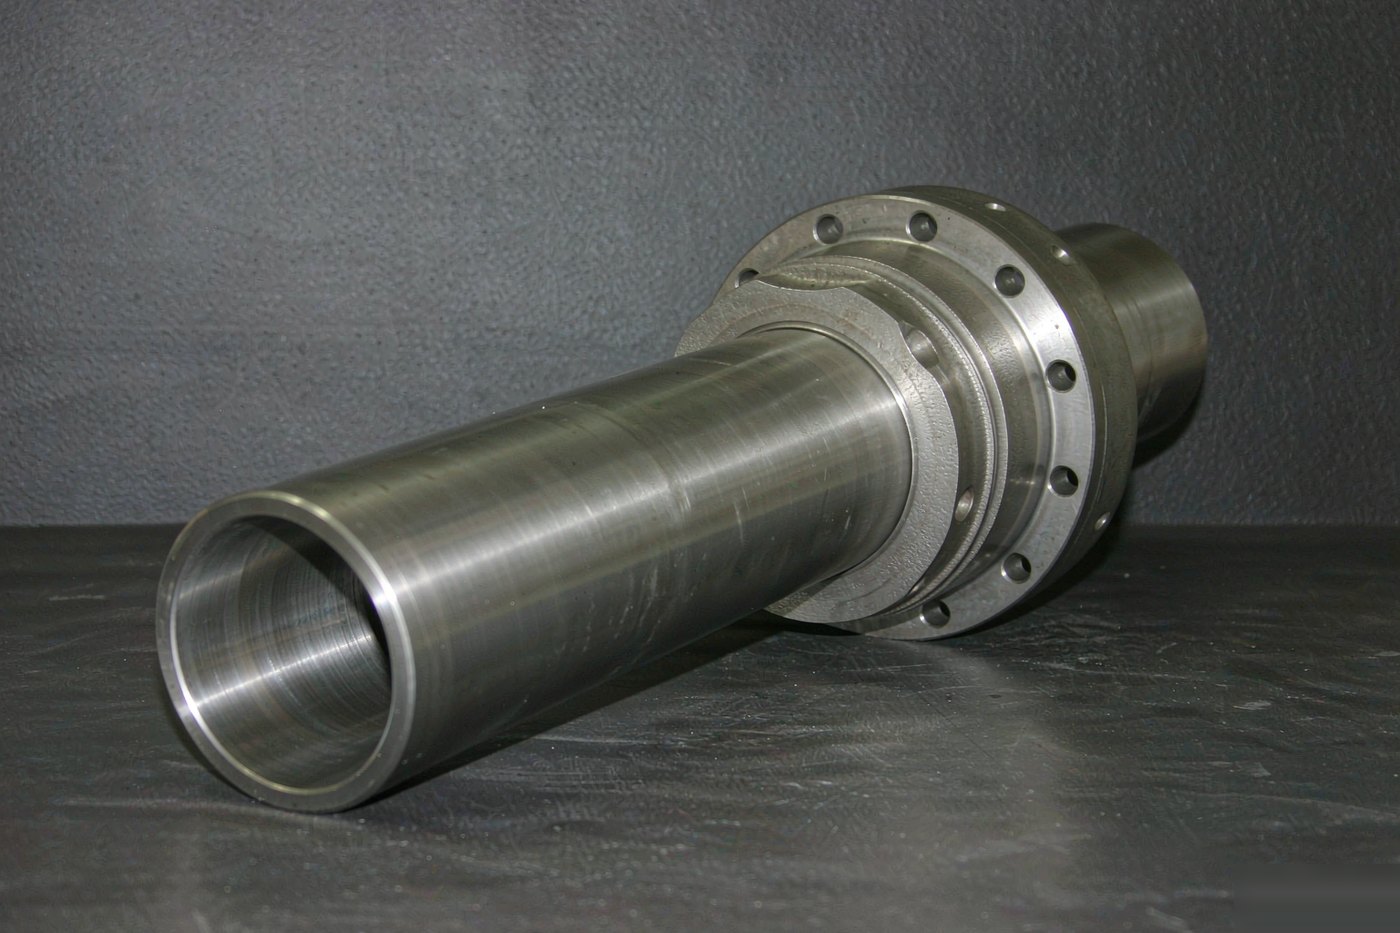
Hardened bore for commodity and engineering resins without aggressive fillers.
View details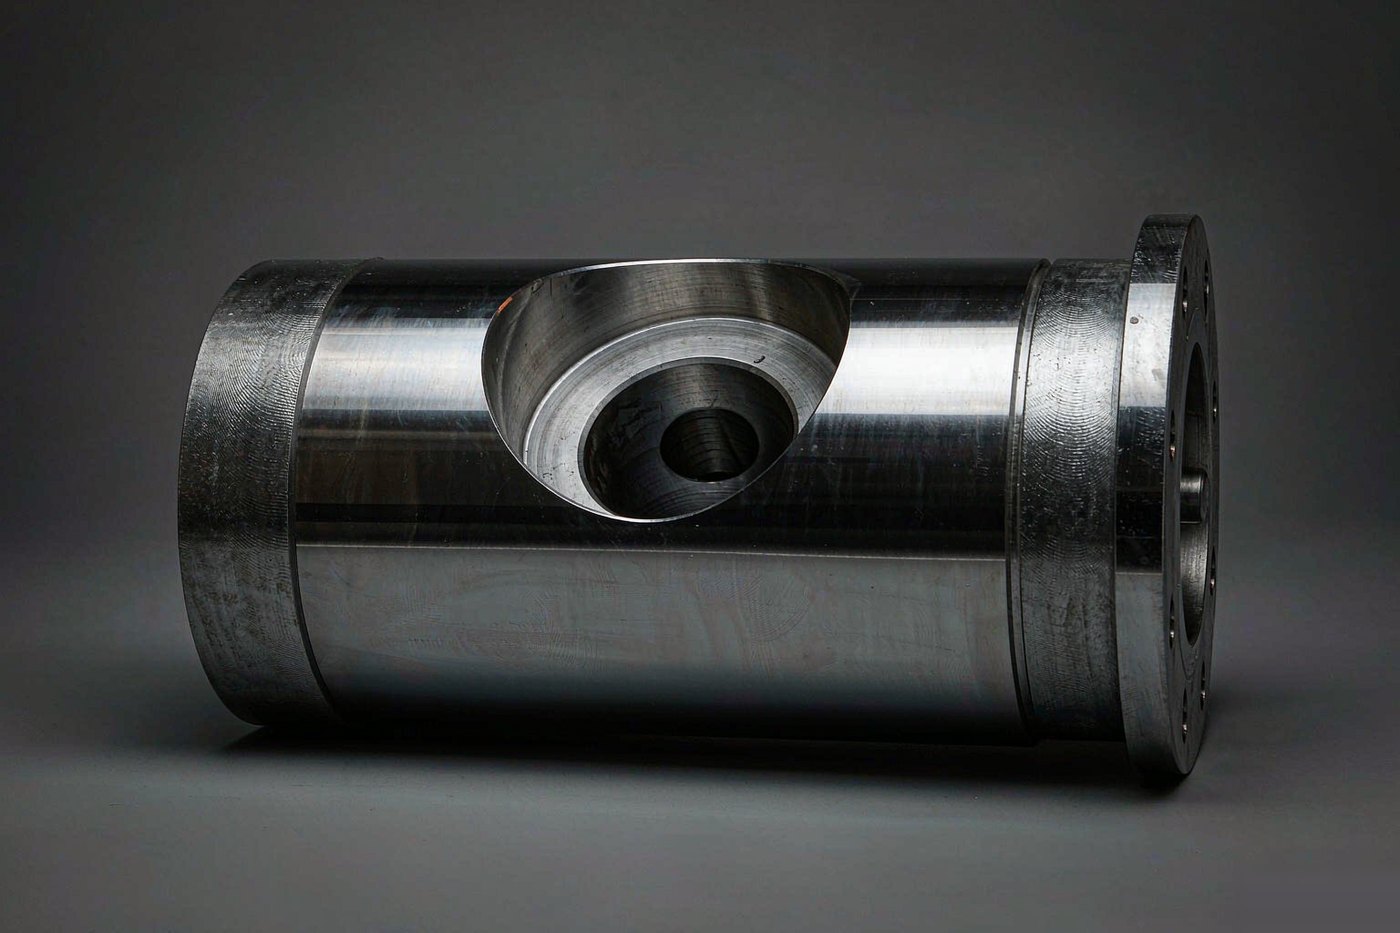
Vent port and decompression zone for hygroscopic and recycled material.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.