
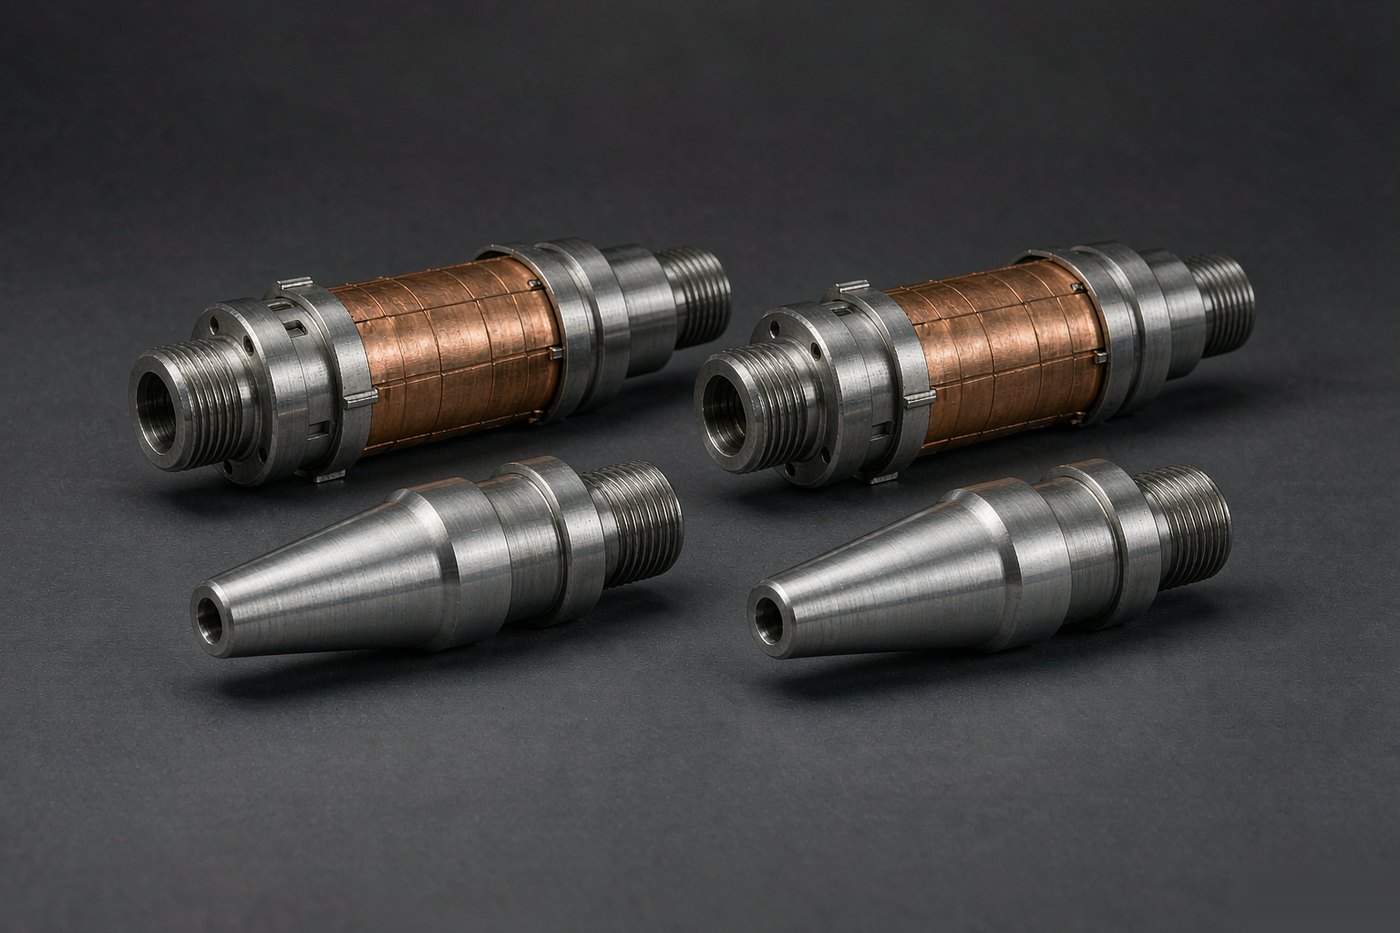
Nozzle Bodies, Adapters and Tips
Nozzle bodies, replaceable tips, adapters and mold clamps in standard and special sizes, matched to your machine and mold.
View details
Nozzle bodies, replaceable tips, adapters and mold clamps in standard and special sizes, matched to your machine and mold.
Machined to your barrel dimensions and screw geometry — no catalogue constraints. Single replacement part or production batch.
Engineering review Monday to Saturday. Send the machine model, screw diameter and resin — the reply carries price, material grade and lead time.
No drawing on file? Send a photo of the worn part and the machine model — we work the geometry back and confirm it with you before machining.
The nozzle is the last place the melt is controlled before it enters the mold, and the first place a cold slug forms. Orifice size, land length and the way the tip seals against the sprue bushing decide whether you get a clean break or a string.
We supply bodies, tips and extensions to match the machine and the tool, in the thread and seat form your barrel end uses.
| Part | Function | Selection notes |
|---|---|---|
| Nozzle body | Carries the melt from the barrel to the tip, often heated | Length set by the gap between barrel end and mold; heater and thermocouple position matter |
| Open tip | Straight through orifice, no mechanical shut-off | Commodity resins, free-flowing melts; simplest and least to go wrong |
| Shut-off tip | Spring or needle closes the orifice between shots | Low viscosity resins and engineering grades where drool is unacceptable |
| Extension | Adds length between body and tip | Deep molds, or when the barrel cannot reach the sprue bushing |
A larger orifice fills faster and shears the melt less. A smaller one gives a cleaner break but raises pressure and can freeze off on a fast cycle. For filled resins, the orifice has to clear the filler — a glass-filled grade through an undersized tip will erode the seat and then leak.
Orifice diameters and thread forms are set per order against your barrel end. Send the drawing or the worn part and we will match it rather than guess from a size code.
Nozzle bodies, replaceable tips, adapters and mold clamps in standard and special sizes, matched to your machine and mold.
View details
Final section of the melt path, carrying the heater band up to the sprue.
View details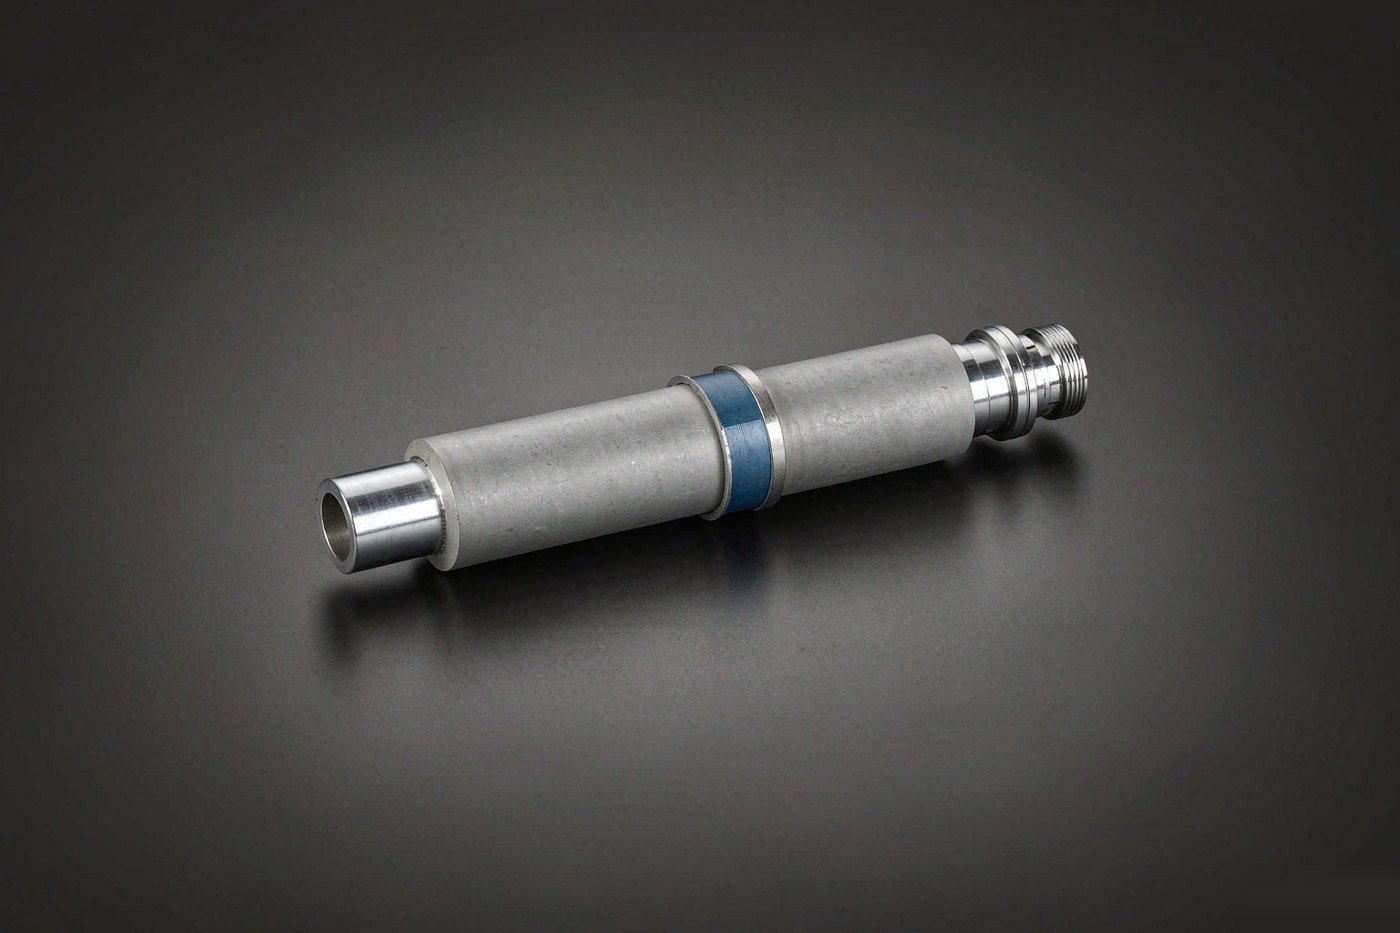
Reaches the sprue when the standard nozzle cannot; heated or unheated.
View detailsSend the machine model and the resin. We confirm geometry, material and surface treatment before quoting.
Have a drawing? Reply to our confirmation email with the file attached — PDF, STEP, DXF or a photo of the part all work.
Our engineering team answers during working hours, Monday to Saturday. For urgent orders, call +8613751260808.